Knowing how to design flex and rigid-flex PCBs is a necessary skill for engineers tackling modern, tight-space electronics. Rigid-flex printed circuit boards (PCBs) integrate rigid FR4 subsystems and flexible polyimide (PI) layers into a single structure, eliminating the need for discrete wire harnesses and connectors entirely.
For space-constrained, high-reliability applications like medical implants, aerospace avionics, and consumer wearables, flex and rigid-flex PCBs remove mechanical failure points that standalone rigid boards with cable interconnects simply cannot avoid. Rigid-flex design carries real business stakes beyond just the technical ones. Material choices, bend radius decisions, and fabricator collaboration – they all affect unit cost, prototype cycle count, and schedule risk.
A design ready for DFM review with the wrong copper type or an under-specified bend radius will require rework, affecting launch timelines and inflating costs. This article will walk you through the distinct methodology needed for such boards.
Standards and Failure Points: Where to Start
Knowing how to design flex and rigid-flex PCBs requires a different methodology from standard rigid design. Generic board requirements fall under IPC-2221, while IPC-2223 covers the flexible sections and the transition zones where rigid meets flex.
When a flexible circuit breaks, it rarely happens randomly. More specifically, a flex board usually snaps or peels due to physical stresses that designers failed to anticipate. Recognizing such physical stresses is the first step in making sure your board actually survives its intended environment. The three failure modes that drive every design decision in this space are:
- Trace fractures in dynamic bend zones from continuous mechanical stress
- Z-axis expansion mismatch between FR4 rigid sections and PI flexible sections during thermal cycling
- Delamination at the transition zone, where flexible material enters the rigid board and stress concentrates
Material Selection: Copper Type and Stackup Construction
Getting materials right is what separates a board that survives 100,000 bend cycles from one that fails during final assembly.
Copper foil is one of the most important material choices in rigid-flex design. Rolled Annealed (RA) copper is preferred for dynamic bending because its grain structure supports better flex life, while Electrodeposited (ED) copper is widely used in standard PCB production and is suitable for static bending or bend-to-install applications. The difference is structural.
- RA copper has an elongated grain structure aligned with the rolling direction, giving it superior fatigue resistance for dynamic applications where the circuit bends repeatedly.
- ED copper has a columnar grain structure that is more prone to cracking under repeated flexing. It costs less and works fine for static bend-to-install applications, but specifying ED copper in a dynamic design invites failure.
One detail engineers frequently miss: an 18 µm RA design can outlive a 35 µm ED design by a wide margin in the same moving application. Ounce weight alone does not predict field life. Because copper type and thickness interact closely, you must resolve both before locking the stackup.
Defining the Rest of the Flex Stackup
Beyond copper, four additional material decisions define the stackup:
- Adhesiveless laminates: Specifying adhesiveless flex cores eliminates a source of adhesive from within the rigid areas and the associated via hole reliability concerns. An added benefit is reduced thickness, improved flexibility, and improved bend reliability. Use adhesiveless construction for any high-density interconnect (HDI) design or tight dynamic bend requirement.
- Coverlays vs. solder mask: Flexible zones require polyimide coverlays bonded with acrylic or epoxy adhesive. Make no mistake, a standard liquid photoimageable solder mask will crack when bent, so keep it restricted entirely to the rigid FR4 sections.
- Polyimide dielectric: Polyimide is the most widely used base material for flex PCBs due to its excellent flexibility, thermal stability, and chemical resistance, and it withstands temperatures up to 260°C.
- Copper thickness: For high-reliability flexible sections, copper thickness should not be selected solely based on current capacity. Thicker copper increases bending stress, so engineers must balance current load, bend radius, flex cycle requirement, and trace width.
Bend Radius: The Numbers That Determine Reliability
Bend radius is the most critical design parameter for flexible circuits. Get it wrong, and copper traces crack, coverlays delaminate, and circuits fail.
IPC-2223E defines minimum bend radii based on application type and layer count. The formula is straightforward: multiply the appropriate ratio by the total flex thickness (including copper, dielectric, adhesive, and coverlay), then add a 20–30% margin for manufacturing variation. Always measure from the inside surface of the bend.
Minimum Bend Radius Multipliers per IPC-2223E
| Layer Count | Application Type | Multiplier (x Total Flex Thickness) |
|---|---|---|
| Single-layer | Static | 6x |
| Dynamic | 100x | |
| Double-Layer | Static | 12x |
| Dynamic | 150x | |
| Multi-layer (3+) | Static | 20x to 25x |
| Dynamic | 200x (consult fabricator) |
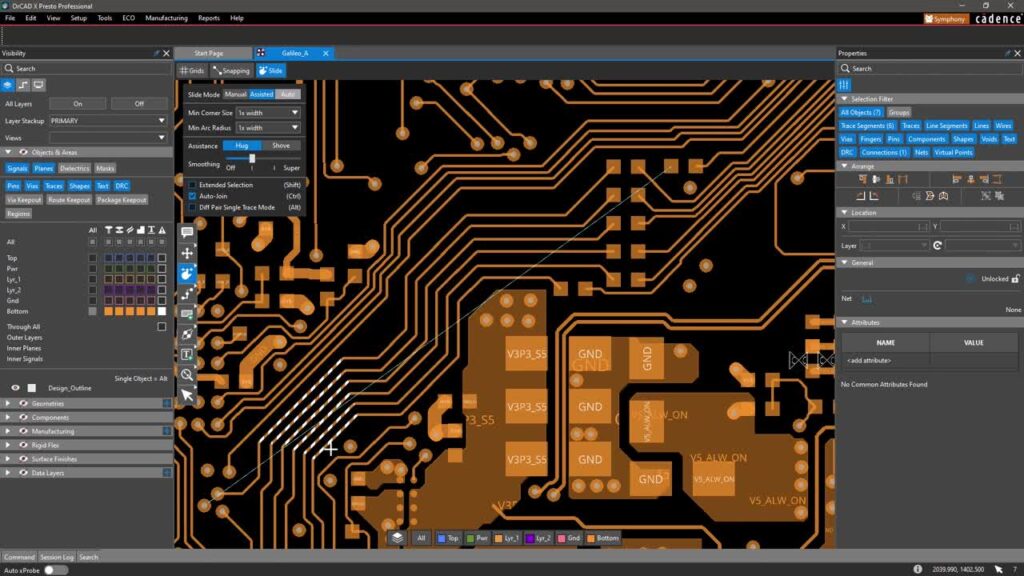
These calculations can be automated and verified in OrCAD X, which supports zone-specific stackup definitions and flags bend-radius violations based on your defined flex thickness natively inside the layout environment, eliminating the need for manual spreadsheet checks before DFM review.
Bend Zone Routing Geometry
Routing geometry inside the bend area is just as important as the radius number itself:
- Perpendicular routing: Traces must cross the bend line at 90°. Angled routing creates uneven stress distribution along the conductor, accelerating fatigue.
- Staggered traces: On multilayer flex, aligning traces on opposite layers directly over one another creates stiff beams that cause stress concentrations. This is the “I-beam effect,” and it will stiffen your flex zone far more than the additional copper thickness alone. Stagger traces on different layers so they do not overlap in bend zones.
- Via exclusion: IPC-2223 recommends excluding vias from bend areas. The plated barrel creates a stress concentration that leads to cracking under repeated bending. If vias must be near bend zones, use teardrop pads and additional plating, but relocating vias to stiffened areas or rigid sections is the preferred solution.
Navigating Layout: How to Design Flex and Rigid-Flex PCBs
Electrical performance and physical limits clash constantly in flex layouts. Let’s face it, a beautiful signal path means absolutely nothing if the board snaps in half. Because every routing or placement choice carries a physical consequence, learning to design flex and rigid-flex PCBs means recognizing that you cannot treat electrical and mechanical limits as independent problems.
Component Keep-Outs and Mechanical Stiffeners
If components are located in areas where the board will bend, solder joints can weaken. To help with weakened joints, consider adding stiffeners if components must be near a flex area, and place components on the stiffeners to prevent mechanical stress. Notably, the rigid-flex transition line is not a soft boundary; treat it as a hard keep-out for all components and plated through-holes.
Geometry and Signal Integrity Across Flex Regions
Managing return paths in flex areas requires a specific approach:
- Cross-hatched ground planes: Solid copper planes restrict flexibility. Instead, use hatched ground planes rather than solid copper in flex regions. Use of hatched ground planes reduces copper content, maintains mechanical compliance, and still provides a reference plane for controlled impedance.
- Teardrops at all junctions: In a flex PCB, a trace entering a pad creates a weak spot where the copper may eventually fracture. Taper the pads down near the end where they connect to traces. Teardrops at every trace-to-pad and trace-to-via connection prevent mechanical cracking at what would otherwise be a sharp stress riser.
- Impedance continuity at the boundary: Because the dielectric constant of polyimide differs from FR4, and because cross-hatching alters the effective return path geometry, trace widths often need to transition at the rigid-flex boundary to maintain a continuous impedance profile. For that reason, always calculate these width changes using your specific stackup measurements.
DFM Practices and Fabricator Collaboration
Rigid-flex manufacturing carries a cost premium over standard rigid construction due to complex lamination cycles. Such design-for-manufacturing (DFM) practices reduce the overall cost of fabrication without compromising reliability:
- Minimize flex layers: Minimizing the flex layer count to one or two layers has multiple advantages, including improved flexibility, tighter bend capabilities, and reduced cost. As a general rule, push additional routing into the rigid sections.
- Use bookbinder construction selectively: The bookbinder construction, where flex layers remain unbonded in bend areas, allows multilayer flex to achieve bend radii that would otherwise cause layer separation. Reserve this bookbinder construction for geometries that genuinely require it, as the fabrication complexity adds cost and lead time.
- Engage your fabricator during stackup definition: Confirm material availability, verify that your dynamic bend radius calculations match their manufacturing tolerances, and ensure they support adhesiveless cores. For designs that call out a specific number of bend cycles, get material and construction inputs from the flex circuit supplier and cycle-test the flex circuits as part of the design approval process. After all, discovering a tolerance mismatch at the DFM review stage is expensive, but discovering it at prototype bring-up is worse.
Early fabricator engagement is one of the highest-leverage schedule interventions available. A 30-minute conversation with your flex supplier during stackup definition routinely eliminates one to two prototype rework. It also surfaces material lead-time constraints before they become critical path problems. Build fabricator review into your design gate criteria, not as an afterthought after layout is complete.
Allegro X provides an integrated DFM check environment for rigid-flex designs, allowing teams to validate layer count, bend zone routing rules, and via placement constraints before releasing Gerbers to the fabricator. Running these checks inside the tool rather than at the vendor shortens the review cycle and reduces the back-and-forth that typically adds days to DFM turnaround.
Pre-Release Rigid-Flex Design Checklist
Use this checklist before submitting for DFM review or prototype fabrication:
Materials
- RA copper specified for all dynamic bend zones
- Adhesiveless laminate specified for HDI or tight-radius requirements
- Polyimide coverlays specified for flex zones (no liquid solder mask in flex regions)
- Copper thickness validated against bend radius and flex cycle requirement
Bend Radius
- Minimum bend radius calculated using IPC-2223E multipliers for layer count and application type
- 20-30% manufacturing margin added to calculated minimum
- Radius measured from inside surface of bend
Routing and Placement
- All traces in bend zones routed perpendicular (90°) to bend line
- Multilayer traces staggered to avoid I-beam effect
- No vias within bend zone (or teardrops and additional plating specified if unavoidable)
- Cross-hatched ground planes in flex regions (no solid copper pours)
- Teardrops applied at all trace-to-pad and trace-to-via junctions
- Impedance widths recalculated at rigid-flex boundary for polyimide vs. FR4 dielectric
Component Placement
- No components or PTHs in flex bend zones
- Rigid-flex transition line treated as hard keep-out
- Stiffeners specified where components are near flex region
DFM and Fabricator
- Fabricator consulted on material availability and adhesiveless core support
- Dynamic bend radius calculations confirmed against fabricator manufacturing tolerances
- Bookbinder construction evaluated and justified if specified
- DFM checks run and reviewed before Gerber release
- Bend cycle test plan agreed with fabricator for qualifying designs
Ready to optimize your rigid-flex workflow? Now that you know how to design flex and rigid-flex PCBs, you need ECAD tools that handle complex 3D stackups and bend zones natively. Contact EMA Design Automation today to discover how our industry-leading flex design solutions can help you prevent mechanical collisions and verify your IPC-2223E compliance before your first prototype is ever fabricated.
EMA Design Automation is a leading provider of the resources that engineers rely on to accelerate innovation. We provide solutions that include PCB design and analysis packages, custom integration software, engineering expertise, and a comprehensive academy of learning and training materials, which enable you to create more efficiently. For more information on how to design flex and rigid-flex PCBs and how we can help you or your team innovate faster, contact us.